Hey folks, gSender 1.6.3 with a number of fixes, behaviour improvements, and features.
Here’s what’s included in this update
New stuff you can use
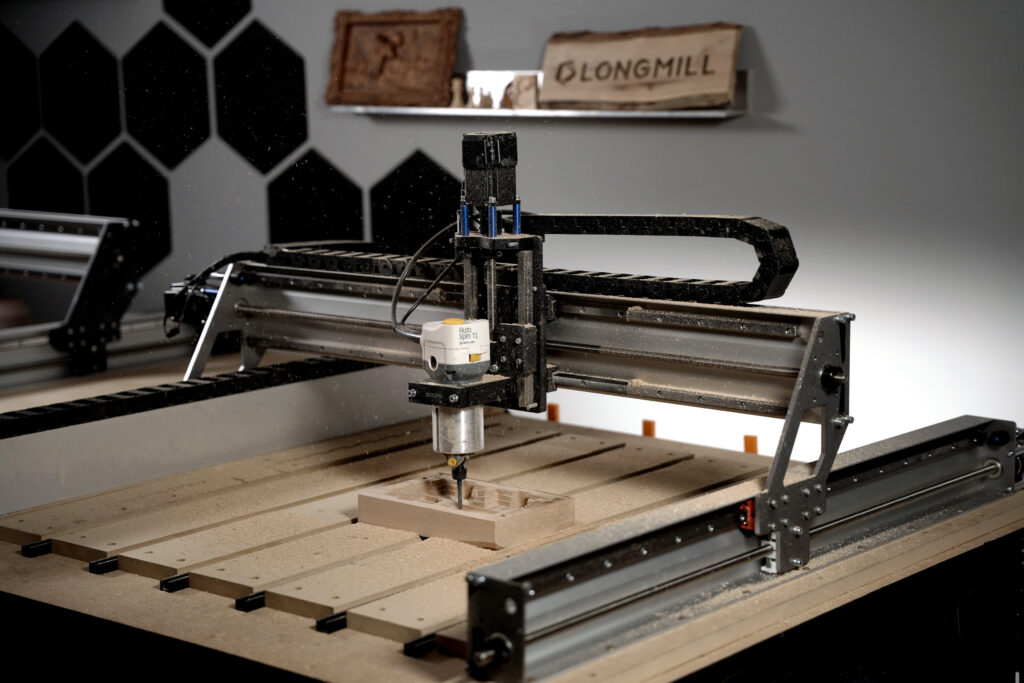
Support for the new LongMill MK3 profiles.
A new flashing option for the upcoming SLB-Lite using UF2
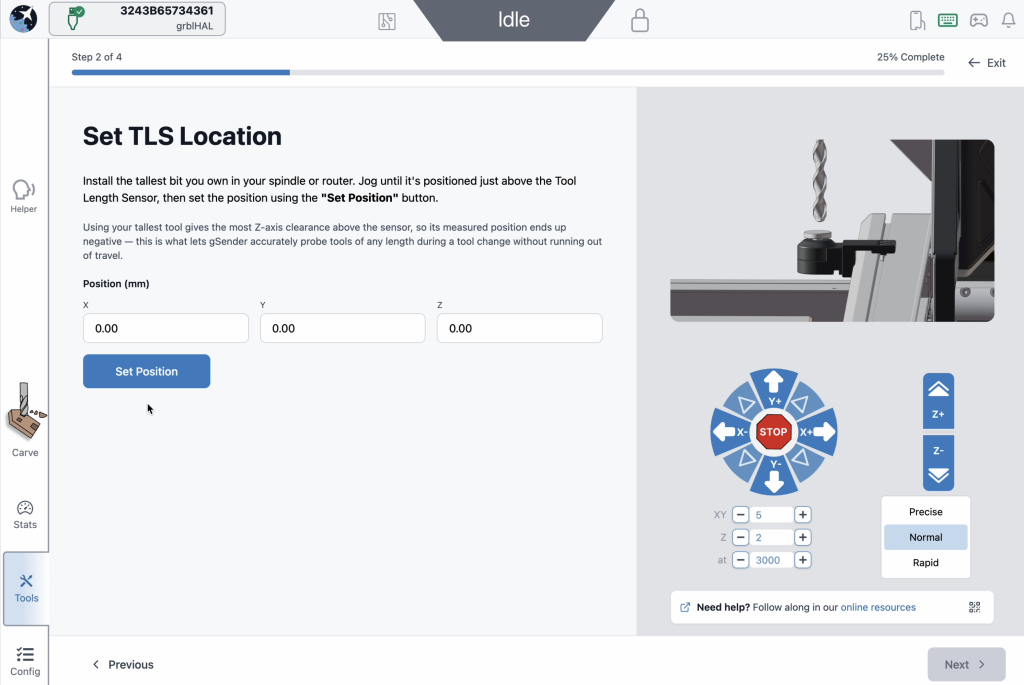
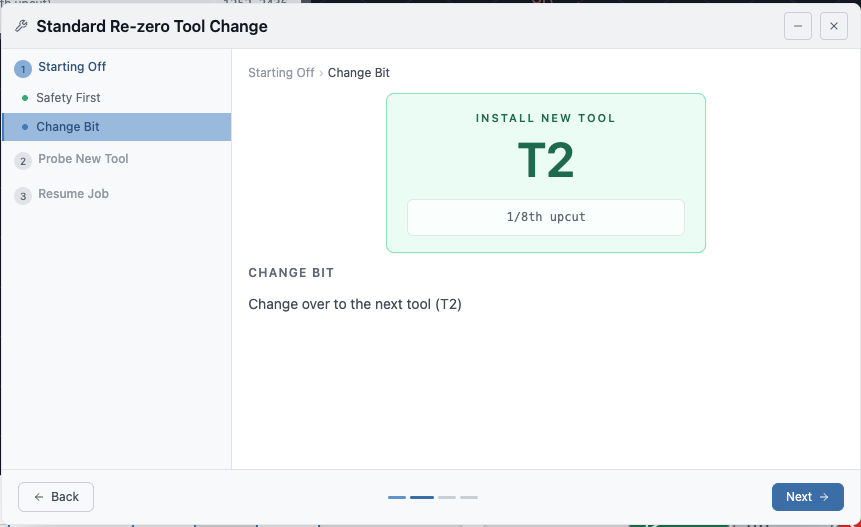
A new TLS installation wizard, found in the Accessory Installation tool. It walks you step by step through picking your probe locations and setting up your toolchanging routine.
#image_title
You can now set a custom feed rate for the final probe movement, instead of it always using the default Rapid speed.
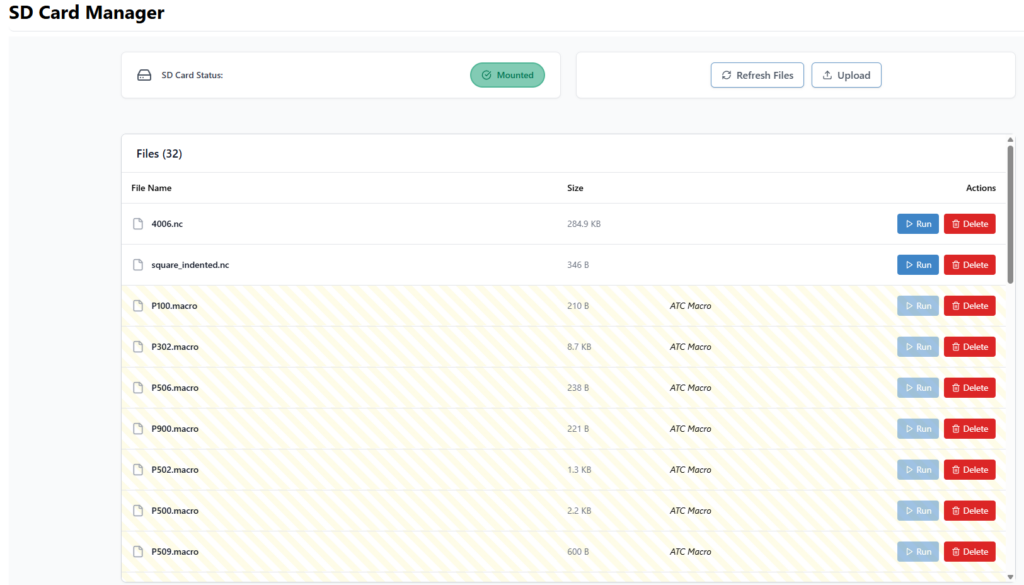
The SD tool now lets you upload several files at once instead of one at a time.
The toolchange wizard now shows a “pending” state while it’s finishing up moves, and it pops up a little closer to when the actual tool change happens, so it feels more natural.
Smoother and more reliable
Changing toolchange or passthrough Config settings now applies right away, no more reconnecting or reloading your file.
Fixed a laser/PWM issue so it works properly without unexpected spindle behavior on grblHAL
Feeder Position variables pos{axis} and mpos{axis} are now always converted to millimeters, even if your machine is set to report in inches (13=1)
Homing status shows up more consistently for machines that are already homed when you connect.
Tool Timeline Probe status now considers non-0 values probed, not just negative values.
Job progress is easier to read with a new background behind the line count.
Made several changes to prevent your Config settings file (sender_rc) from getting corrupted, and if it somehow does, the app will no longer fail to start.
Firmware profile updates
Updated to support the latest grblHAL firmware, including changes to how lasers and PWM work.
Bugs squashed
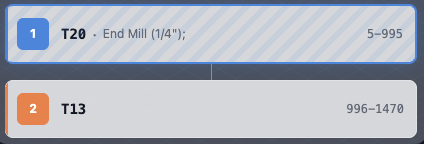
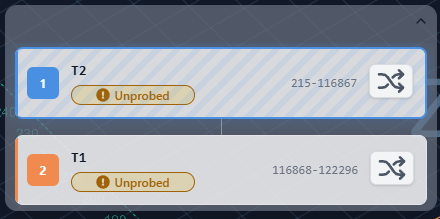
Fixed the tool timeline showing the the original, non-remapped value when minimized
Fixed a probe dialog bug where connectivity tests would falsely show as passing if enabled when opened
Fixed a display issue in the Config tool when undoing changes to certain values.
Fixed the single-axis homing toggle appearing when homing disabled.
Fixed the park shortcut to worked when the firmware reports homed status
Fixed job progress not updating properly after tool changes pausing progress.
Full Changelog
Added LongMill MK3 profiles.
Added flashing path for new SLB-Lite using $UF2.
Added TLS installation wizard to the accessory installation tool.
Added ability to specify feed rate on final probe movements — default 0 continues to use G0; any other value uses G1 Fx where x is the configured value.
SD tool now allows uploading multiple files at the same time.
Added pending toolchange state to the toolchange wizard while already-planned lines finish their motions, and delayed wizard appearance until closer to the actual M6 command.
Updating the toolchange passthrough setting now updates the controller without reconnecting or reloading a file.
Updating the passthrough setting in Config updates that option without requiring a file reload or reconnect.
No longer swaps spindle min/max for grblHAL, so PWM can be used as a laser without issues.
pos{axis} and mpos{axis} feeder variables are now always returned in mm, regardless of report-in-inches ($13) status.
Homing status on connect for already-homed grblHAL devices is now more consistent.
Tool probe status now allows positive values — only 0 is considered unprobed.
Probe status badge in the tool timeline now only shows when using grblHAL with ATC=1 (tc.macro exists).
Added background to job progress line count for readability when the visualizer is disabled.
ATC options tool is now disabled if no SD card is mounted.
Improved reliability of Config Store truncation.
Added various updates to prevent the ConfigStore file (sender_rc) from becoming corrupted.
Corrupted ConfigStore files no longer block application startup.
Various firmware updates for the latest grblHAL core version.
Updated grblHAL profiles for the new firmware release — mostly related to laser/PWM2 behaviors.
Entering laser mode on grblHAL no longer swaps $30 and $31 with the laser equivalents.
Fixed tool timeline not reflecting the remapped tool number after minimizing.
Fixed issue where opening the run probe dialog with connectivity would cause all future connectivity tests to pass immediately.
Fixed issue where restoring an altered EEPROM value in Config without applying wouldn’t update the UI with the correct value in the Config tool.
Fixed toggling single-axis homing on and then off in the on-state not showing the original “go to” buttons.
Fixed backwards logic on the park shortcut, allowing usage when homed.
Fixed job progress not updating correctly after a tool change was handled via one of the wizard strategies.
As always, thanks for your continued support and feedback. If you run into anything unexpected, let us know!
Another busy June has come and gone. Welcome to our latest update!
Employee Appreciation Day
Lead Times For Major Products
AltMill 2×4 and 4x4s are now shipping quickly, typically in 2 weeks or sooner. We have stockpiled some assemblies and full machines to help keep our lead times low.
Batch 2 of 4×8 machines are now in production, and we are expecting units to start shipping in August.
All spindle kits (minus the ATC) are now shipping within 2 weeks as well. We are now in production of Batch 2 of ATCs; new orders being placed now are expected to ship in August-September.
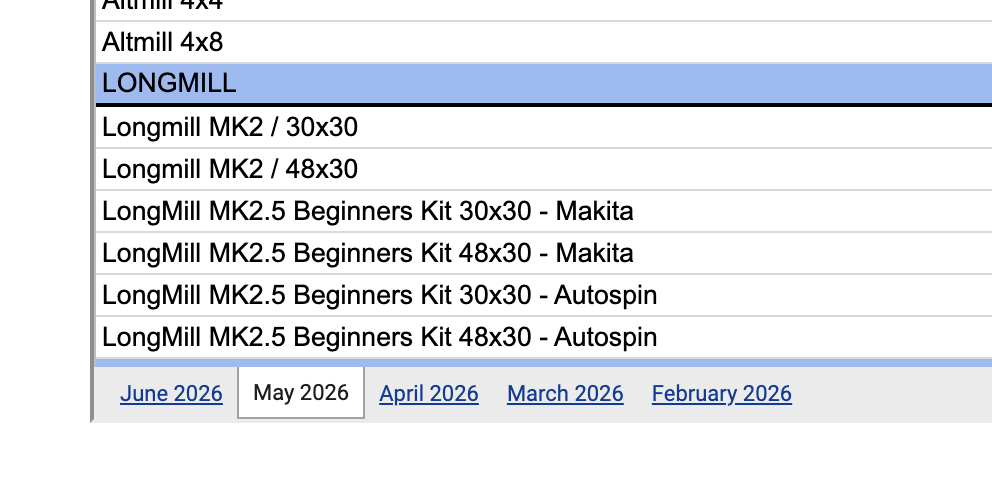
For orders that have already been placed, please refer to the estimate provided in the month/week that you ordered the product. Please note that the lead times that are presented on the product page only refer to orders placed at that time. Your order lead time will be different if you have already placed an order in a prior month.
You can see the tabs for each month at the bottom of the sheet on the Order Status page
LongMill MK2.5s are shipping within 1 week, and LongMill MK3s are also expected to start shipping in September.
For the latest list of shipping timelines, please check out our Order Status page.
Catching up on Maintenance Stuff
The last few months have been pretty busy with new product launches, but now that we’ve gotten through all of the big things, you should expect to see a bit of cleanup on our end, including:
Updates and cleanup to resources and documentation
Updates and cleanup for open source files and documentation
Uploading of maintence and replacement parts on our store
Continued training for our customer support team
Continued improvement in gSender, our firmware and other parts of our ecosystem
Development of ancillary technologies and products, like a CNC control pendant, sensorless homing motors and vacuum workholding
I don’t think I can list every single little detail, but users should expect to see small changes come down over the next few months.
Tool Length Sensor
Although we’ve mentioned this a few times in saying that gSender fully supports a tool length sensor, and users can/have installed a tool length sensor on machines with aftermarket TLS, we have now finally made the TLS sensor available to all users.
As you may know, the Auto Tool Changer system requires a TLS system, so we designed a TLS sensor specifically for our machines and systems.
Benefits of the Sienci Labs TLS:
Greatly improves productivity for CNC projects that use multiple cutting tools by removing the need to manually re-zero each time the tool is changed
Break-away magnetic interface prevents damage to tools or machine in the event of any errors during tool length probing
Hardened 45HRC 4140PH probe disc ensures a durable tool probing surface and makes certain wear does not affect probing accuracy
Optical sensor provides high accuracy and repeatability, unaffected by temperature like other sensors
Flexible mounting allows the sensor to mount directly onto your AltMill or LongMill, or other CNC other machines.*
Last month we launched the LongMill MK3. We have continued to work on the production for the machine in anticipation of shipping in September this year. Most of our work has been in finalizing some of the mechanical design and pushing to production our fast turnaround parts.
Additionally, we have been finalizing our packaging design with plenty of destructive drop testing.
We also had a livestream to talk about LongMill MK3 engineering, design, philosophy, and more, so if you want to check that out, see below:
SLB-EXT V2 and SLB-LITE
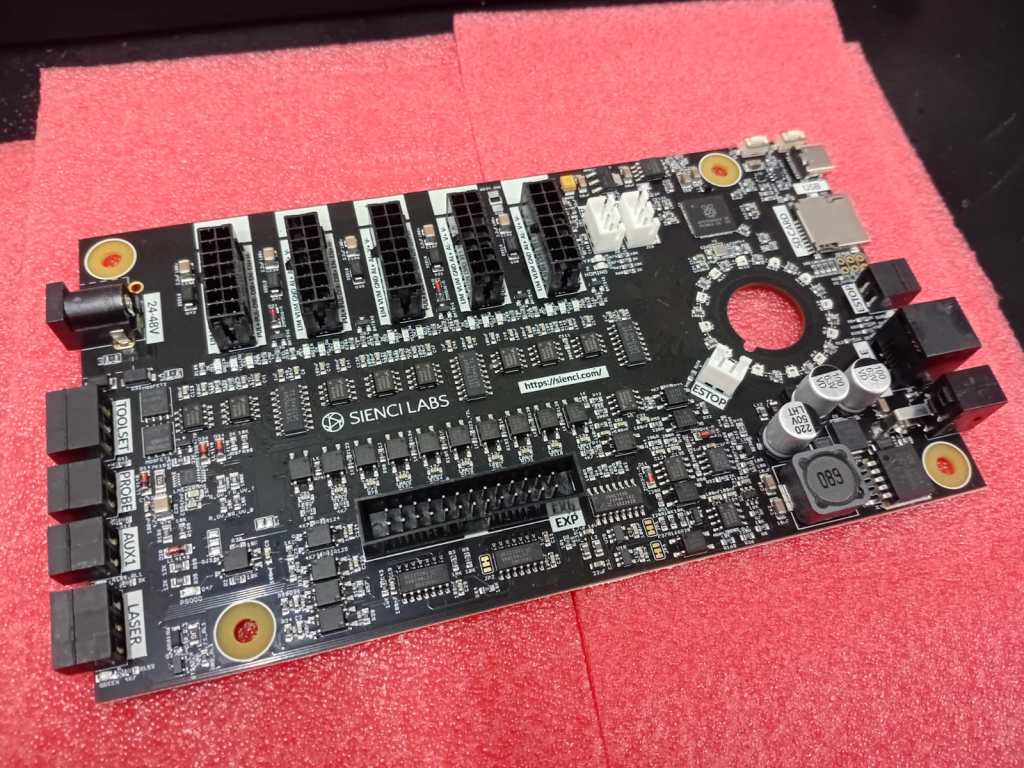
First test cuts using the SLB-LiteFirst batch of fully populated next gen SLB boards!
We have continued to make progress in the second generation of SLB-EXT controllers. We have now received another 20 units of samples in early June for continued testing. Here’s some general work
Continued work on the firmware configurator tool to allow for users to customize their firmware for their needs
Minor fixes to board design and components (namely the fit and sizing of the power connector in this case)
Testing of signal consistency and noise
Real life testing and cutting with SLB-LITE
Work on the expansion board for further functionality
Looking at noise on the 5V regulator
Pricing Changes to gControl Panel Computer
Due to continuing instability in the cost of processors and memory, we are again increasing the price of the gControl panel computer. We are continuing to negotiate with our suppliers, but we expect that pricing will be updated for the following batch of units.
Pricing is expected to be updated as following: USD $529 / CAD $739. Please note that timing of the change and final pricing may vary over time.
As we’ve mentioned in prior updates, we do acknowledge that the cost of the computer is high, and so we are actively working on a longer term computing solution to bring the same or similar functionality at a lower price. This is not to say that the gControl panel computer is overpriced. In fact, for a industrial level, fanless panel computer, it’s quite inexpensive, but we do recognise that not all users need such an overkill piece of hardware.
Testing the budget version of “gControl”
Sensorless Homing
In a bid to reduce component count, reduce costs, and improve overall reliability, we are currently undergoing testing and development in sensorless homing technology in conjunction with our R&D with close-loop stepper motors.
Because of a closed loop motor’s inherent ability to detect when a motor loses steps, we can also use this feature to understand when a motor has reached the limit of its travel. In a traditional machine, a separate homing sensor or switch is used, which is triggered when the machine hits a limit. However in a sensorless homing setup the motor is used to detect the limit. A closed loop motor can do this because there is an encoder and electronics inside that compare the amount of rotation the controller has commanded it to turn versus the amount it actually turned. When there is a mismatch, the motor knows that it’s “lost steps”.
To make sensorless homing work, we need to tune and program the motor to improve the sensitivity of the motor, so that it can detect contact with the machine faster and more accurately. We can do this by varying the amount of power going to the motor, the speed, microstepping, touch off distance, filtering algorithms and more. Additionally, we need to consider the mechanical structure of the contact points.
While this is a bit of a tricky thing to get right, this technology has been proven to work very well in modern 3D printers, to the degree that most 3D printers rely on this technology alone for their homing sequence.
The advantages of sensorless homing is that we remove one of the potential weak points in the machine design, which is the homing sensor. While homing sensors are extremely reliable, due to the added complexity of installing them, the wiring, and the additional hardware, we believe that reducing component count can improve the overall reliability of the machine in the long run. Additionally, while the cost of the switches are fairly low, the cost reduction in removing the ancillary hardware, instructions for installing them, configuration, and more, we believe that we can see some decent cost savings overall.
Naturally, people are going to ask if their existing machines will be able to support sensorless homing. With some generations of motors, it is possible. However this does require re-flashing the motors and may require special tools. If your machine is working well with homing switches, it’s unlikely to be practical to move to a sensorless homing system and there is no practical performance differences when both systems are working well.
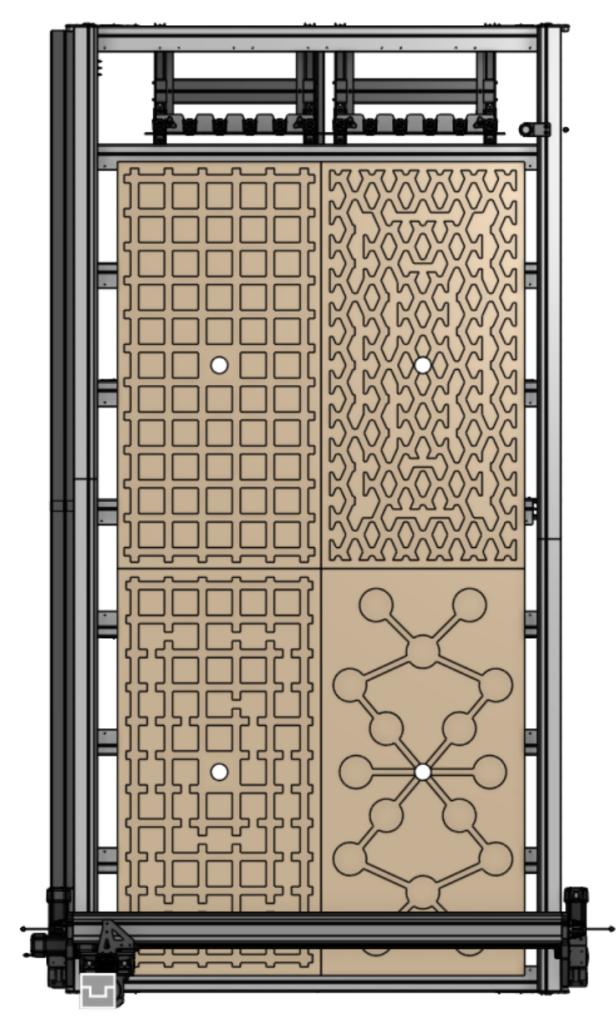
Vacuum Table Development
Over the last few months, especially coinciding with the AltMill 4×8, we’ve been working on a vacuum table solution in the background. As we continue to work on more advance systems focused on more professional level applications, we naturally looked to adding a vacuum table system to our machines.
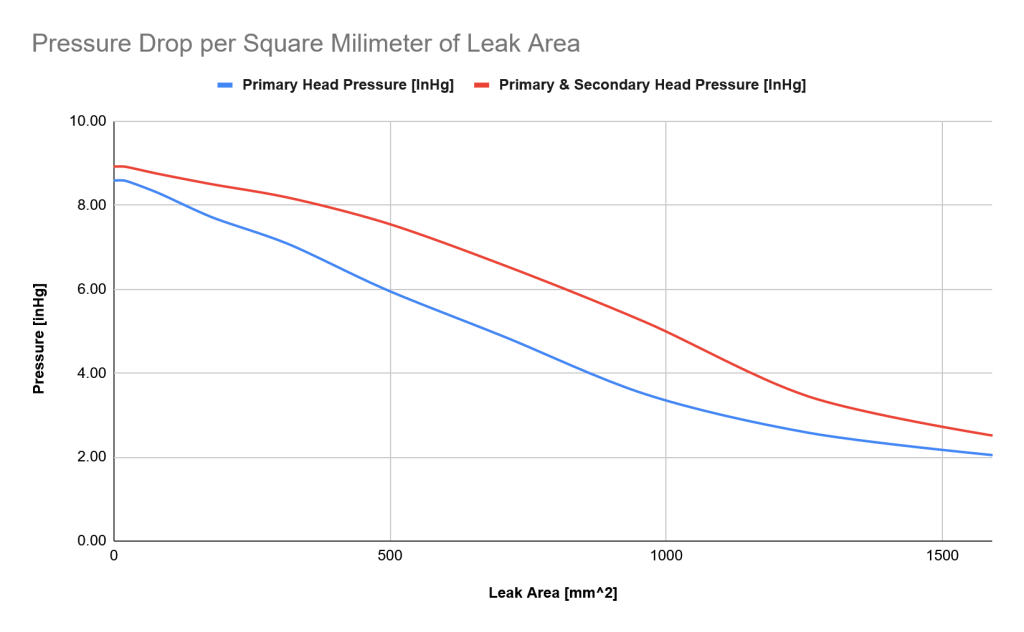
Test patters for vacuum holddownTesting data for vacuum table designs
Most of our work is currently exploratory, trying to understand:
What sort of vacuum pump and architecture we should use
How much performance we need and how much performance we can get in different configurations
Potential shipping and logistics processes
Sienci Labs will be at IWF Atlanta
We will be at IWF Atlanta! We are working on the planning and logistics for coming down, but we’ll be bringing a few team members down to show case some of our cool products and chat with members of the community.
IWF Atlanta is one of, if not the largest woodworking fairs in the world.
If you’d like to attend, make sure to check out https://iwfatlanta.com
Hey everyone, welcome back to our June 2026 production update!
More Open Positions at Sienci Labs
We have a couple official positions now posted on Indeed as we continue to grow our team. With continual expansion plus the development and release of new products, we’re constantly looking for new people to join our team.
We also have a few positions likely to come online in the coming months as well, including people to join our engineering team for hardware and electronics, additional software developers to focus on gSender development, and an in-house CNC instructor.
If you want to reach out to us because you feel like you could be a good fit with our company, please feel free to submit through our general application form.
Changes to Website Coming Soon
Ever since our beginning, our development on our website has been shared between a few different people in the company, but we never had a dedicated web developer on the team. But now, with the recent addition to our team to work on our website, you can expect to see some updates and changes coming down the pipeline. Our main focus right now is improving the user experience on the customer service side through our Contact Us page, plus the Resources to make it easier to find information faster.
Test siteExample wireframes
LongMill MK3
The LongMill MK3 has now launched! If you want to learn more about it, read our article.
In other news, we’ve been continuing to work on a few things this month, including:
Continual design and testing of packaging
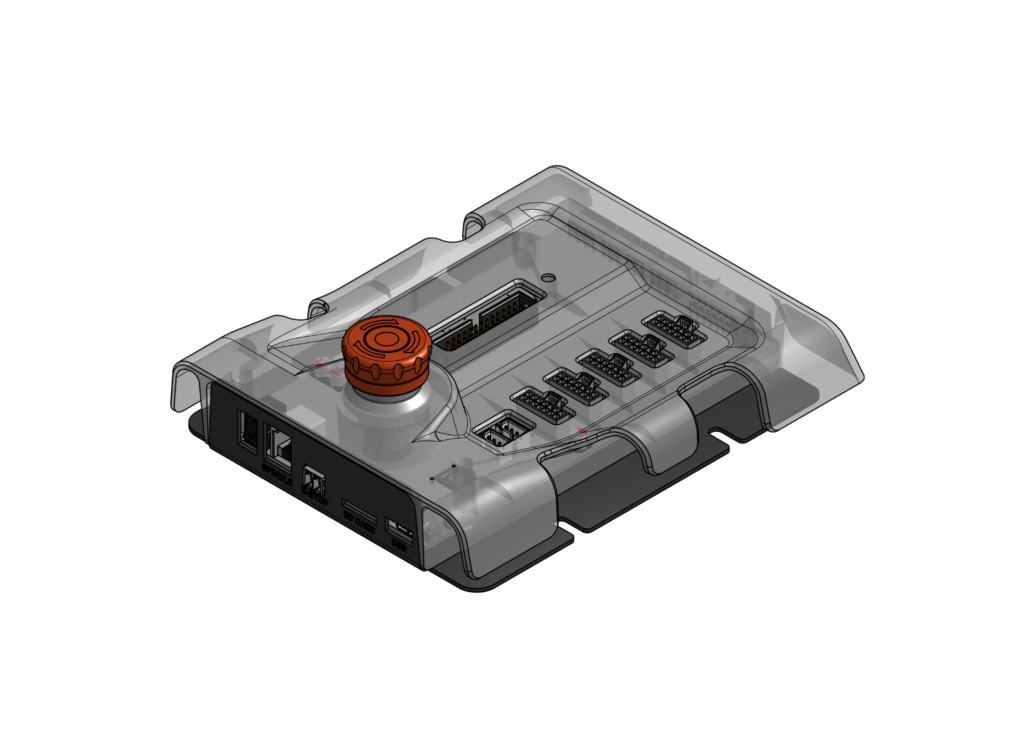
Development of the SLB-LITE
Machine testing
Dust shoe design and testing
SLB-LITE and SLB-EXT V2
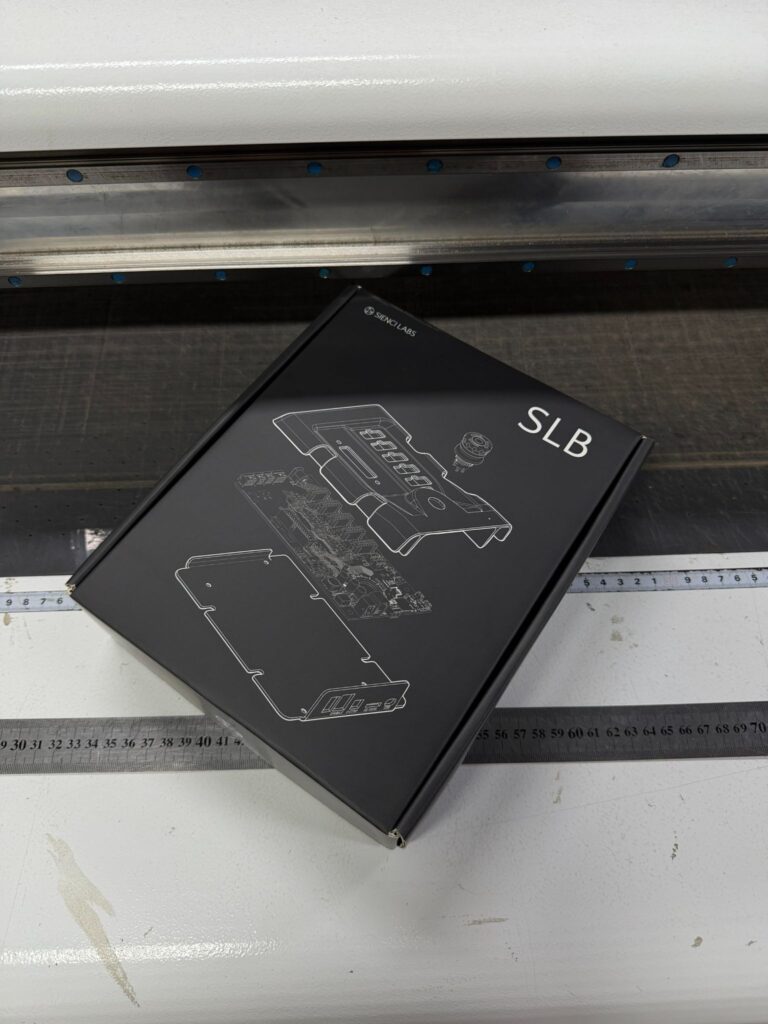
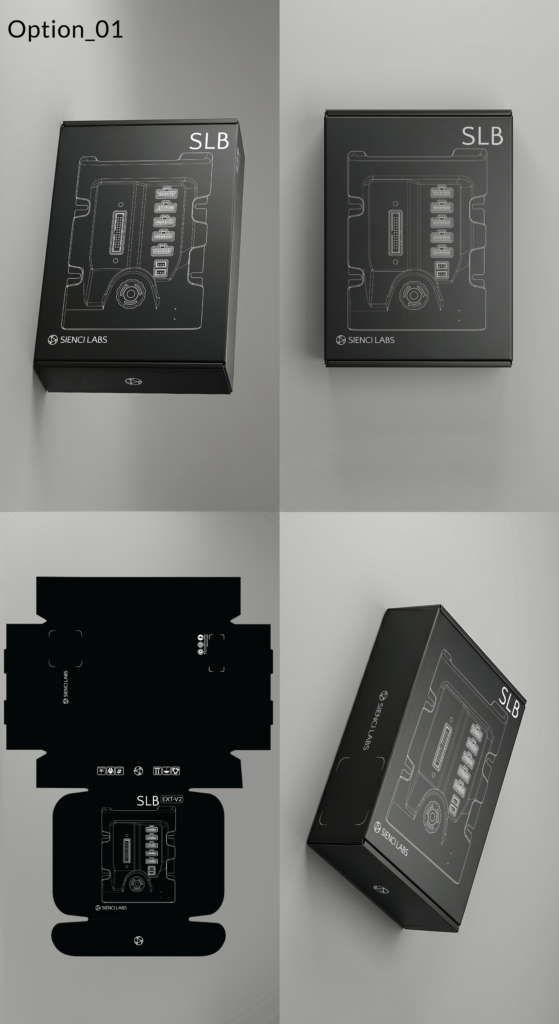
Packaging samples for the SLB-EXT V2
A lot of work done on the new generation of SLBs, including:
New samples of the packaging
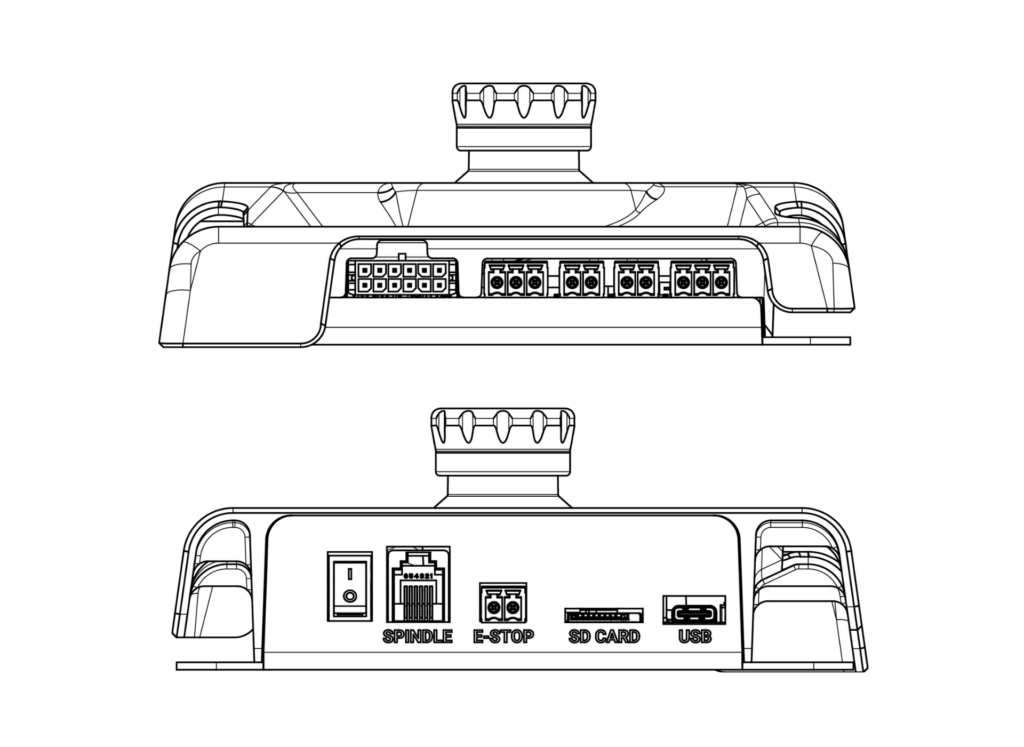
Testing and development of key features, such as the RGB LED support, Ethernet communication and board expansion design
Reliability testing with early prototypes
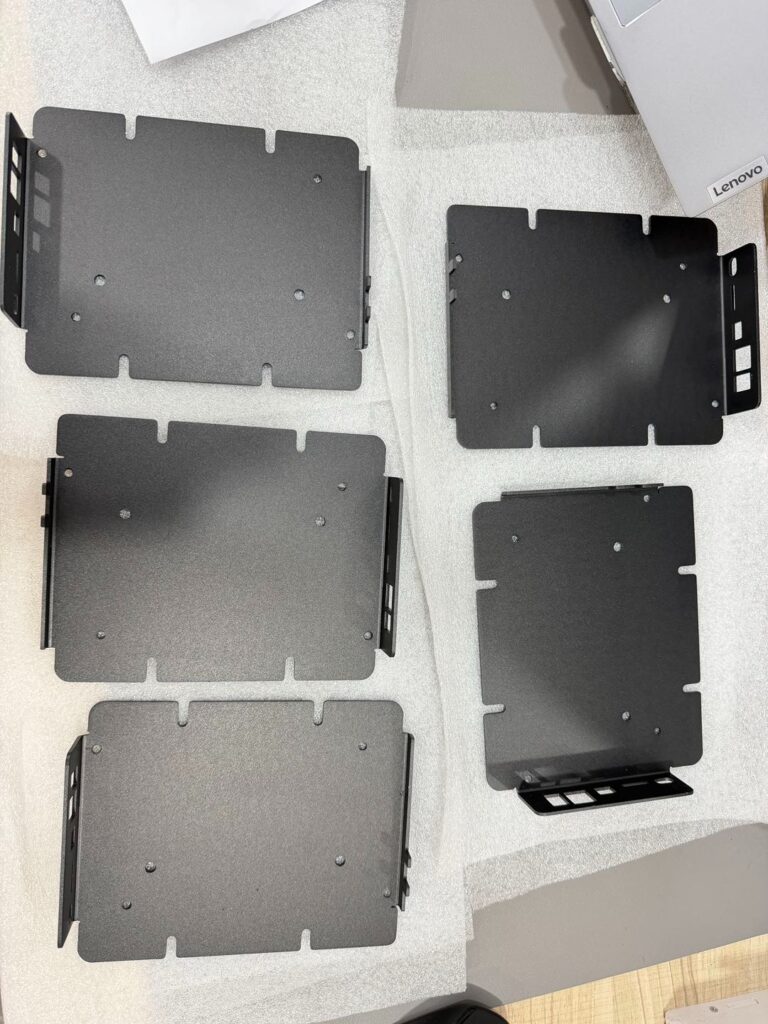
Manufacturing of key components, such as the front and back plates of the controller enclosure
Back panel samples
AltMill 4×8
As mentioned in our last update, we’re in the process of ordering another 300 machines for the new batch. Otherwise we’ve been continuing to do long term accelerated wear testing for the AltMill 4×8, essentially running the machine constantly back and forth 100,000 times at high speed and acceleration, with sudden stops and starts. For context, this is a super extreme condition and we expect no one to ever come close to running it at these conditions.
Here are some of the findings:
Change in backlash is essentially non-existent, under 2 thou
Motors heat up to 92C, which is close to the 90C limit that the gearbox can handle
Besides the bearing retaining ring on the gearbox starting to come loose, all other components are still at the torque they need to be
Overall, this means:
Under normal operating conditions, it’s unlikely for users to see any significant decline in performance or accuracy
Motors only heat up to their limit at the most extreme conditions
We can reduce the chance of the bearing retaining ring coming loose with adding some locktite during assembly. However, given that the machine was run at extreme conditions where the amount of vibration is significantly higher than normal operating conditions, we believe that this is not an issue. We will include in maintenance documentation for users to check the ring during regular maintenance. The good thing is also that when this item becomes loose, it is visually obvious, which makes it easy to address if needed.
Clear Cut Dust Shoe
When we first launched the Clear Cut Dust Shoe for the 80mm spindles, we didn’t anticipate how popular they would be. We had originally set aside around 100 dust shoes for individual sale, which were all sold within a few days. The remaining dust shoes have been set aside to include with the Spindle Kits for the LongMill and AltMill.
We are expecting some more dust shoes to come in in 2 weeks and another batch in August. We will announce very shortly when they will be available again for single purchase.
Spindle Lead Times
Spindle lead times have been long for the past few months, as we received more orders specifically for the 1.5KW spindles than we were expecting. We’re happy to announce that a new batch of spindles have come in and we are working through backlogs. Please check the orders status page for the latest lead times.
Some Interesting Proof of Concept Projects
If you’re interested in knowing what else we have going on, we have a few “proof-of-concept” projects that we worked on in the past month. These are projects that don’t have any commercial direction at the moment, but highlights our interest in pushing the technology further and could be things you may see in the future. We have a lot of different “proof-of-concepts” that we work on, but these were two that I thought were particularly cool.
Perhaps it’s also worth mentioning that when you buy stuff from us, a lot of that money goes back into R&D to develop products and updates that benefits the ecosystem as a whole, so remember that it’s not just an investment you’re making today, but it can impact what your machine and the machines of others can do in the future.
“Autofeedrate“
One of the challenging things with setting up a CNC for cuts is figuring out the speeds and feeds. With the implementation of “autofeedrate”, we can actively adjust the feedrate in real time based on the load on the spindle. In essence, we can take a current reading from the spindle cable and adjust the feedrate down to optimize the load on the spindle in relation to how much material it is cutting. This means that if there’s more cutting capacity that the machine can handle, it can automatically run faster. Or, and likely more important to the average user, reduce the feedrate before the spindle can stall.
In industry, this is a feature that is used to optimize feeds and speeds in manufacturing, where shaving seconds off the cycle time can result in significant cost savings in a production facility. However, the implementation of this technology can cost thousands, if not tens of thousands of dollars.
The use of autofeedrate in a hobby level setting, on the other hand, would allow users to reduce the amount of guesswork required to set feeds and speeds on their machine, especially due to differences in material, machine, and tooling differences. In essence, one of the challenging parts of providing a streamlined experience in CNCing is the fact that there are so many variables to take into account. By having an active system in monitoring load and adjusting for these factors could help optimize cuts and reduce the knowledge needed to operate a machine.
The exciting part of this technology is that the hardware and sensors needed to implement this can be done on most existing machines and are fairly inexpensive ($20-50). The software and signal processing is the more complicated and expensive part.
gSender on CM4
Up until recent months, gSender has been a fairly processor-intensive program. With recent improvements to gSender, we’ve managed significant speed and reliability improvements. However, we mostly see and expect users to run the program on full scale computers and laptops.
Kevin (one of our senior software developers), has been working on a new proof of concept we are expecting to funnel into a wider development of a more affordable control panel to control grblHAL machines.
To be frank, a solution like the gControl Panel Computer, is expensive for the average hobby user. While we see a big chunk of AltMill users buy the gControl Panel Computer, very few use it with a LongMill. I suspect this has mostly to do with the market that we are serving with the LongMill since it is a lower cost machine.
So what is the gSender on CM4? CM4 is a compute module, or a single board computer. They are generally cheaper than full size computers ($30-100), and are designed more for embedded applications and for light computing. Oftentimes, a CM4 is used as a development platform for testing before going into a full integrated computer design, as they are easy to set up and can be purchased off the shelf.
Since something like the CM4 has much less processing power than something like the N150 Intel processor found in gControl. This means gSender for CM4 needs to be optimized for that level of processing without losing functionality. This proof of concept shows the screenc apture of an optimized version of gSender designed for CM4.
One of the key things to note is the redesign of the UI, which is made to be touch screen friendly and work on smaller screens. In the long term, we expect to implement this solution into a computer that can act as an affordable controller or pendant so that users don’t need to plug in a laptop or buy a gControl for their machine.
gSender 1.6.2 is a smaller follow-up release focused on polishing up some edge-case issues that cropped up after 1.6.0, along with a number of workflow and usability improvements across the application. A lot of this work targets firmware compatibility, ATC/tool change flows, and smoothing out a few rough edges reported by the community over the last little while.
Data collection and analytics
You may also notice that gSender prompts you again about analytics/data collection preferences after updating. If this feels familiar, you may have already responded to this prompt quite a while ago and simply forgotten about it. We’ve recently changed analytics providers, so we wanted to give everyone another opportunity to review and update their preferences.
The data collected is primarily general usage metrics, operating system information, and tool usage data that helps us understand what parts of the application are being used most often and where issues may be occurring.
As always, analytics participation is completely optional and can be enabled or disabled at any time in the Config section of the application.
General Fixes and updates
Updated firmware defaults to better account for TLS/probe misconfiguration scenarios
Various firmware default updates and compatibility improvements for newer firmware versions
Uploading to SD cards over ethernet is working correctly again
Laser power slider now behaves as expected on newer firmware
Spindle selector now works correctly on newer firmware
Laser offsets now map correctly to the updated Config key structure
Flash utility will now automatically select grblHAL firmware when SLB_DFU is detected
Exiting rotary mode will once again properly restore previous machine values
Non-enabled spindles will no longer appear in the spindle dropdown list
Spindle dropdown will now attempt to refresh itself automatically if empty in the Spindle/Laser drawer
UX and Visual
Numerous visual and workflow improvements to the tool change wizard
New Wizard
Tool change wizard will now resume the spindle before returning to the previous XY position.
Tool change wizard and tool timeline now display annotation comments when no ATC nickname is set
Parsed Comments
Removed probed/unprobed status on firmware versions without a tool table
ATC Config will now store default values on first install instead of stored values
ATC Config will now warn in situations it failed to read the stored configuration file.
Squaring and motor tuning workflows now share the same jog popover for a more consistent experience
Spindle delay behaviour has been updated and is now an explicit configurable option for forced insertion when needed
Functionalities
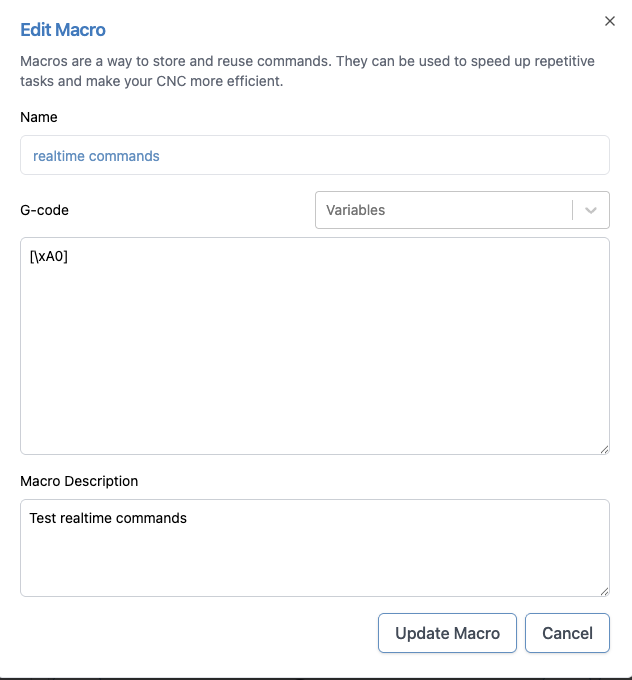
Macros can now send realtime commands using the [\xNN] format
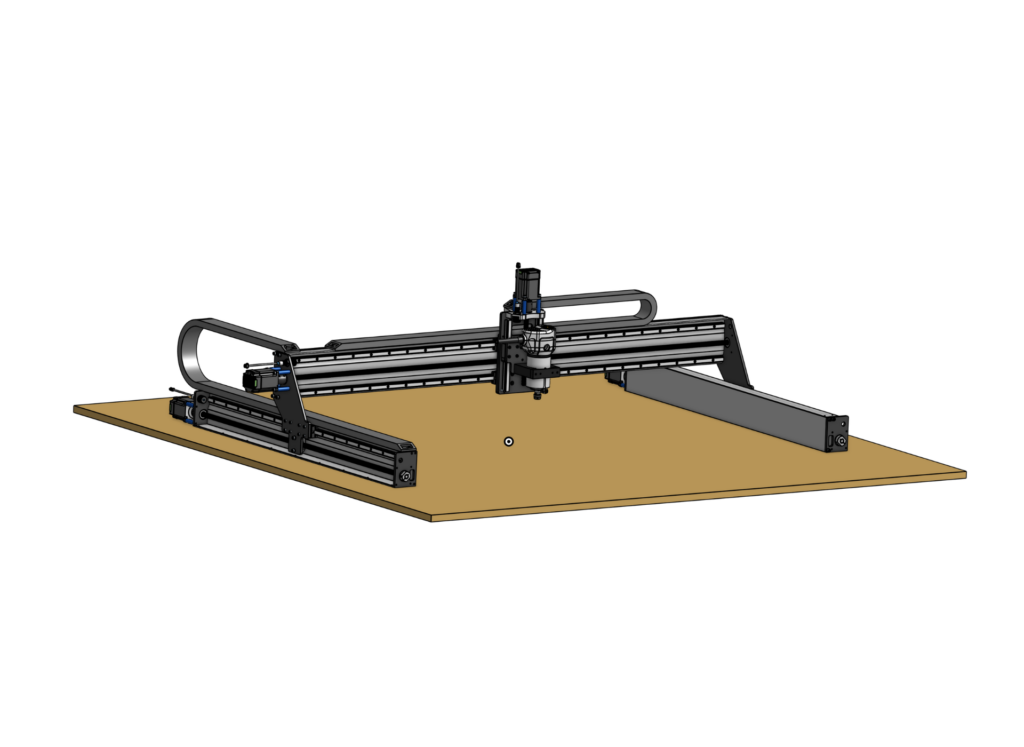
The LongMill MK3 is the successor to our past line of LongMills. Like the original LongMill, its aim is to provide a beginner friendly experience to people who are looking to get into CNCing, while providing enough power and performance to be a productive machine. The LongMill MK3 was designed to address several of the LongMill’s weak points, integrate new technologies, optimize manufacturability and ease of assembly.
To speak frankly, we designed and we believe that the LongMill MK3 lineup represents the best entry level hobby CNC under $2000USD in terms of performance, design and customer support. We are excited to launch the LongMill MK3, as it represents a huge step forward in the hobby CNC field industry.
Addressing Weak Points in the LongMill MK2 Design
Having shipped over 10,000 LongMills to date, we’ve experienced the impact of many of the design decisions made for our outgoing model, which has helped shape the design of the new LongMill MK3. Here are some of our learnings and takeaways.
V-wheels. While V-wheels are cheap, forgiving, and generally easy to use and maintain, they come with several drawbacks. First is that they require regular adjustment. The user must maintain a specific amount of tension to ensure that there is no play in the machine movement. This level of variability leads to variance in cut quality and tolerance. The use of linear guides, more specifically the HR15 type linear guides and blocks which are also used in the AltMill does not require adjustment and inherently has very little play, allowing for a more rigid machine. This system does have a small but reasonable drawback, which is that the linear guides must be oiled regularly. However, from our experience with the AltMill, this process is simple and easy enough that the process is easier than maintaining v-wheels.
Lead screws and ACME nuts. The ACME lead screw system on initial MK1 and MK2 LongMill designs also required user adjustment. In this design, the user uses a screw to adjust for backlash in the Delrin nut threads by pushing two halves of the thread apart. This also required the user to regularly adjust as the threads would wear. With the MK2.5 design, we implemented spring loaded anti-backlash nuts to the existing lead screw system, which eliminated the need for this adjustment, as the springs would automatically take up slack as the nuts wore down. We chose to stick with the ACME lead screw system over a ball screw system, largely due to cost. A ball screw system requires additional bearing blocks and hardware, and generally does not allow us or the user to cut the rails and lead screws to different lengths to allow variations in sizes like the LongMill does. The existing lead screw system is more than precise enough for the application and allows us to keep the LongMill MK3 at a lower price point.
Open-loop steppers. Due to the nature of open-loop stepper motors, when the LongMill stalls or misses steps, the machine continues cutting, making it difficult to salvage projects. The use of closed-loop steppers means that the machine can detect when it’s lost its position, so that it can pause the cutting job and allow the user to rehome and restart the machine. Closed-loop stepper motors are generally also more efficient and can run faster with more torque, which means that we can run the LongMill MK3 faster and harder than the LongMill.
Implementing New Technologies
The development of the AltMill has allowed us to “trickle down” some of the parts and innovations into the LongMill MK3. While HR15 Linear Motion components are more expensive than v-wheels, due to the larger economies of scale, we are now able to purchase and use them for the LongMill MK3 while keeping a similar BOM price as the LongMill.
Additionally, our work in creating and improving assembly processes allows us to utilize some of those techniques in the LongMill MK3 as well. We also are using the same types of closed-loop stepper motors and the SLB-LITE controller, which is also possible due to the high volumes of motors we are already buying for the AltMill.
Work in features and improvements in gSender and GRBL-HAL also play a key part of the overall user experience with the LongMill MK3, including stronger integration of an independent 4th axis, auto-squaring, gcode editing, granular control of EEPROM settings, and the use of a tool length sensor. While these features are now available for legacy LongMill users, the LongMill MK3 specifically prepares the use of the machine with the new features in mind.
Another key development that was created with the LongMill MK3 in mind is the AutoSpin T1 router. While we’ve been selling and recommending the Makita RT0701 for many years, we developed the AutoSpin T1 to be a successor to it by not only bringing a higher standard of quality and durability, but also the ability to control the router on-off, and speed. Overall, this allows the machine to be closer in functionality to higher end machines that use traditional spindles at a fraction of a cost. The LongMill MK3 was designed specifically with the AutoSpin T1 in mind.
Improving Manufacturability
We’ve made significant improvements to the manufacturability of the LongMill MK3 primarily through reducing the number of unique parts and pre-assembly of certain components.
The LongMill MK3 contains approximately 30 unique components, which is a 25% decrease from the LongMill MK2. We were able to do that by:
Eliminating the need for rail feet by having the LongMill MK3 Y rail screw directly into the wasteboard
Using T12 hardware across all axis, rather than using T8 on some and T12 on others
Integrated mounting points for the drag chains
Integrated motor and sensor cables
While decreasing the bill of materials by 10 unique components might not sound like a lot, this eliminates a lot of work including supply chain and sourcing work, QA, documentation, and even resource development. We are also able to purchase larger quantities of parts, which helps improve our economies of scale and bringing the overall cost of the machine down.
Improving Ease of Assembly
The LongMill MK3 substantially increases the ease of assembly with more of the machine assembled in house. We’ve chosen to move in this direction because:
It eliminates a lot of packaging, as we don’t need to individually pack items into boxes and bags
We can perform more QA checks through the assembly process by ensuring that parts come together with the proper fit and finish
Tools and processes implemented in the production and assembly of the AltMill product line allow us to speed up the process of assembly for the LongMill
We can reduce the amount of development needed for assembly resources
The time that the customer needs to assemble the machine is significantly lower
Like the AltMill line, the LongMill MK3 will be manufactured and assembled wholly in house at our shop in Waterloo Ontario, which allows us to keep a close eye on quality throughout the whole batch.
Additionally, as we mentioned earlier, there are way fewer unique parts, which means that for the parts that the user does need to self assemble, this process will be easier overall. Based on our testing, we expect users to be able to assemble and set up their machines in less than an hour, 2-3 times faster than the outgoing generation.
Competitive Landscape
Since the original LongMill launched in 2019 and especially in the past year, we’ve seen a ton of new launches for beginner friendly CNC machines, some from the Chinese market and some from the North American market.
With CNC technology becoming more accessible and affordable, we’ve seen a lot of growth in the beginner and hobbyist market. This gives us a lot of new insights on what we think works and doesn’t work.
A move away from belts and wheels: Earliest hobby CNC machines used belts and wheels in their motion system. While cheap, these components require adjustment and lack the rigidity that hobbyists expect today.
Pre-assembled/partially assembled machines: Users expect machines to be much easier to assemble, with most machines pre-assembled or partially assembled, requiring the user to only need basic assembly and wiring to complete the machine.
Closed-loop motors: While at the moment, most hobby CNC machines still use open-loop motors, we expect to see a shift towards more closed-loop motors for their performance advantages. As we discussed in the article about the Closed-Loop Stepper Motor Kit for the LongMill MK2 (https://sienci.com/2025/12/15/everything-you-need-to-know-about-the-closed-loop-stepper-motor-kit/), we’ve seen prices come down for the components needed for closed-loop stepper motors as they become more popular in CNC machines.
Performance Differences
With the conjunction of closed-loop steppers and thicker lead screws, we are able to push the rapid speeds of the LongMill MK3 to almost double the speeds of the MK2.
LongMill MK2
X and Y default max rapid speeds = 4000mm/min, 157IPM
Z default max rapid speed = 3000mm/min
LongMill MK3
X and Y default max rapid speeds = 7000mm/min, 275IPM
The performance of any CNC machine depends a lot on the overall rigidity. Based on our testing, we are able to see between 60 to 80% improvement in overall rigidity of the machine. This means that not only can the machine move faster, it can handle the extra power. In practice, this means shorter cutting times, cleaner results, and more reliability overall.
Comparison at 25N/5.62lbs
Positive X (thou)
Positive Y (thou)
LongMill MK2 48×30 (extrapolated)
7
10
LongMill MK3 48×30
4.5
8
Difference (thou)
2.5
2
Difference (%)
64.29%
80.00%
Comparison at 50N/11.24lbs
Positive X (thou)
Positive Y (thou)
LongMill MK2 48×30
14.2
20.7
LongMill MK3 48×30
10
11
Difference (thou)
4.2
9.7
Difference (%)
70.42%
64.29%
Pricing
Pricing and sizes for the LongMill MK3 series will be approximately the same as our prior generation machines:
LongMill MK3 30×30 ~$1400USD or $1890CAD
LongMill MK3 48×30 ~ $1800USD or $2430CAD
We’ll once again be offering a bundled Beginner’s Kit, which will include the AutoSpin T1 router, an AutoZero Touch Plate, a dust shoe and some end mills, This bundle will offer savings around $100CAD/$110USD vs buying these accessories separately.
Please note that pricing may change slightly at launch/production.
Production Schedule
Pre-orders are expected to open up May 26, 2026 at 11AM EST.
When pre-order opens we will share an expected shipping date, which is looking like mid-to-late August, possibly early September (at the time of this Blog). We are currently in production for 1000 units.
Stay tuned for announcements in three weeks.
FAQs
Will I be able to upgrade my LongMill MK1, MK2, or MK2.5 to the MK3? Practically speaking, no. The LongMill MK3 is a complete rework of the design and so the cost difference between buying a new, full machine and doing an upgrade would be negligible.
Can I use a spindle with my LongMill MK3? Yes, you can use the same spindle kit that we currently offer for the LongMill MK2.5 on the LongMill MK3 with essentially the same installation instructions. It should be noted that since the spindle is larger, users may lose some travel in the X.
If I buy a 30×30, can I upgrade to a 48×30 later? Yes, we will make the parts required to increase the size of the X axis to turn a LongMill MK3 30×30 to a 48×30 available. However, we do not currently have specific plans to have them available at the time of launch.
What is the difference between the LongMill MK3 and the AltMill? We built the LongMill MK3 with entry level/beginners on a budget in mind. The AltMill is aimed more towards pro-sumers and semi-industrial use. For a full comparison, check out our video:
Is the LongMill MK3 compatible with the Makita RT0701? Yes it is, and all LongMill MK3s will come with a 65mm mount. Please note that you may need to use an extension cable for the Makita RT0701 to pass through the drag chains.
Does the LongMill MK3 support Sienci Labs’ accessories? Yes, any accessories from the LongMill MK2.5 and prior will work with the LongMill MK3, with the exception of dust shoes, which have been design specifically for each machine.
Can you tile/pass sheets through the back of the machine? Yes, just like all other LongMills, the rear of the machine is open and you can pass larger sheets through the machine. It should be noted that you may need to position or route the Y motor cable in a way to prevent interference with material if you do choose to do tiling.
Can you mount the LongMill MK3 vertically? Yes. With the substantially stronger motors and larger lead screws, we expect essentially no performance drawbacks in mounting your machine vertically.
What will support look like for owners of LongMill MK1, MK2, and MK2.5 machines? Support will continue to be largely the same. We have stockpiled between 3-5 years of spare components to support our users of older machines, and open source design files and specifications are available through the respective resource pages of each machine to allow users to source alternative components if necessary. Otherwise, technical support will remain the same between all of the different versions of the machine.
Back in the March 2026 Production Update, we mentioned that we added about 2500sqft of production space to our shop. I’m excited to announce that our office expanded again this month by another 3500sqft. This includes around 2100sqft downstairs, which used to be a large boardroom to be turned into media space, where we’ll use as a dedicated filming space for the marketing team. We’re also looking to potentially host classes and events there down the line as well.
The upstairs ~1400sqft is expected to be used primarily as desk space, with some focus for the customer service team, as the space has a couple of enclosed offices, which should allow them to make and take calls in a quieter environment.
AltMill 4×8 Now Shipping
We are excited to announce that starting April 16th we started shipping the first batch of AltMill 4x8s! A huge congrats to the production and engineering team for working diligently to iron out any last minute QC issues, as well as the customer support, marketing, and resource teams for pulling together the resources for the use and assembly of the machine.
For all of the machines that have been ordered, please check our Order Status Page for estimates on when your machine will ship. We are expecting new orders for the AltMill 4×8 to ship in August, so lead times remain long for the time being. The new batch (batch 2) is expected to have 300 units.
Youtube videos on the complete assembly of the 4×8 are now out, so make sure to check those out!
ATC Now Shipping
Extra exciting news is that the ATC is now shipping as well since April 16th! Again, a huge accomplishment for all of the teams at Sienci Labs for pulling off what is probably our most complicated project to date.
Our first batch of ATCs have sold out, and we are now in production for another batch. We are expecting orders for ATC placed today to start shipping in June. We are nearly sold out on our second batch of ATCs as well. If you order in our third batch, we are expecting those to ship out Aug-Sept. Please see our latest Order Status updates for lead times.
As you may or may not know, we also designed a TLS (tool length sensor) for the ATC process, but we’ll have those for sale to accompany regular spindles as well, so keep an eye out for that. This has been a feature a lot of people have been asking for.
Videos for ATC are also now out, so feel free to check those out as well!
gSender and Firmware Updates
There is a new major release of gSender! Check out the full blog post here: https://sienci.com/2026/04/16/gsender-1-6-0-release/. gSender 1.6.0, now the latest version of gSender comes with a huge number of improvements, such as faster loading times, a built in gcode editor, and new EEPROM settings manager, but also comes with new features required for operation of the ATC and AltMill 4×8 functions. This also aligns with updates to the firmware coming out, mentioned back in January. We are shipping machines now with the new firmware to ensure ATC support, and users will be provided with resources for updating their machines to new firmware in the ATC resources.
LongMill MK3 Development
LongMill MK3 development continues to chug forward. Most of our work this past month was tweaking the design, general testing, packaging design, and planning for the resources development. As mentioned at some point in one of the updates, we are expecting to open pre-orders late May, with shipping expected to start around mid to late August. Keep an eye out for the “Everything You Need to Know About the LongMill MK3” blog releasing this week as well.
A couple of key directions we’re looking to go down at the moment include:
More of the machine pre-assembled in house, which means faster set up time for the end user
Streamlined packaging, since less bags and boxes required when parts are already assembled into units
SLB-LITE/SLB-EXT V2
Development continues to move along for the SLB-LITE and SLB-EXT V2. We have now been doing testing and troubleshooting for the new boards for the last few weeks and working on tweaking the design for the second version.
Things done this month include:
Design and production of pulp molds for packaging
Ordering of mounting bushings and other parts needed for case assembly
Ordering of e-stops
Initial test production batch of 200 PCBs, and if no issues, we’ll push for the full batch (around 1000 controllers)
Otherwise we expect to be continuing testing and design work for the new controllers into May and June.
1.6.0 was well received (thanks for all the feedback), but a few issues and edge cases popped up across different setups that we wanted to address quickly. 1.6.1 is focused on tightening things up, improving consistency, and smoothing out some rough edges.
Changes
Added option to skip the first tool change when using fixed strategy, with a prompt to confirm
Added application scaling support for larger monitors and devices (Config → Accessibility)
Hey all, Chris here. It’s been a while since I’ve posted on the Blog, the last time was actually when we launched the LongMill MK2.5 which was posted nearly 2 years ago on May 10, 2024, so I hope my writing doesn’t come across as too rusty.
I’m glad to be writing to you all again, though in this case this will be the last time, as I wanted to let you know that I’ll be leaving Sienci Labs both as CTO and co-owner to begin a new chapter of my life. In light of this, I felt there was no way that I would be able to leave without at least attempting a final walk down memory lane so I could share with you some of the impacting experiences and community moments that stood out to me. So, if you’ll indulge me, I’ll do my best to capture these even though we all know there’s no way I’ll be able to summarize 10 years of all the time, energy, and passion I’ve put into building Sienci Labs from the ground-up, as well as all the time I’ve shared with so many of you through support emails, Facebook comments, Forum threads, calls, in-person meetups, Livestreams and more.
Before starting down memory lane though, here are some other housekeeping items that I should elaborate on first:
Why am I leaving? As everyone knows life is complex and always shifting and sometimes you just have to embrace it. After much consideration I felt it would make sense for me to move on to other things at this stage in my life.
Why also leave as an owner? This was the choice that I felt made the most sense. Andy and I both have built this company from the ground-up with no outside investment because we felt that those who own the company should be the ones involved in the day-to-day of building it. Since I was looking to move on, it felt like the right thing to also work with Andy to return all my ownership back to the company.
How will this change things at Sienci? In my view you shouldn’t really see any change. This probably sounds weird for me to say since you’d imagine that one of the key co-founders leaving would make a larger impact, but from my perspective there are a couple key aspects that I feel makes this statement true. Firstly, from day one Andy and I have worked hard to establish and make known the key priorities of Sienci Labs, including community openness, open source, and accessibility, and I believe that by instilling these pillars in our team it ensures that these goals can continue on through each of them. Secondly, as my role at the company has evolved over the years, we’ve already brought on people to fill the gaps to much success between my input or mentorship and their own talents including engineering, packaging design, QA, documentation, marketing, video creation, etc. This past experience allows present-day transitions to happen quite smoothly when there’s good planning and communication. Lastly, to give more context to the second point, recently my efforts at the company have been in projects that have either now released or are shortly releasing including heading the gSender 1.5.0 ‘New U’ redesign, the original board design and firmware behind the SLB and all the related documentation, filling the gaps on the new gSender 1.6.0 release, handling transition back to the core grblHAL firmware, and then onboarding new talent to finish that work and handle future SLB work. This means I’m in a good spot to hand the reins of successful, long-term projects over to either Andy or other talented individuals we’ve brought on, and I have great confidence that they can continue from there.
Should I still keep messaging you about Sienci stuff? Unfortunately no, I won’t be the right person to talk to anymore, but there are a lot of great and knowledgeable people you can always reach through Sienci customer support. We’ll also do our best to distribute this Blog post across our various channels so that people who might’ve gotten a reply from me recently on places like our Forum or Github should know to expect any future follow-ups to come from someone else on our team due to my departure.
What are you moving on to? For now I’ll be taking a very long overdue break as well as looking after some family and friends, then we’ll see from there.
I hope that answers most of the important questions. From my view Sienci Labs is in good hands. The team is strong, the vision is clear, and though I’m sad to say goodbye I wish the absolute best for the company to continue building tools that empower creativity and innovation.
For anyone happy to finish reading here (as I know that the following reminiscing might only be interesting for certain groups of people), my final words would be: have a great week, be well, help others, enjoy CNCing, and remember that feedback will always encourage Sienci and other companies in the space to keep improving! (:
How This All Started
I’m sure that between videos and blog posts, anyone who’s followed our company from the start may already have a decent idea of the path we took to where we’re at now, so I’ll try to offer up some less-mentioned insights from my own experiences.
From my view, the birth of Sienci and its core tenants started from Andy and my immersion and thankfulness to the multitude of prior community-founded efforts towards the democratization and increase in accessibility of at-home manufacturing, and honestly just the broader ‘maker’ movement as a whole. This movement had achieved a much larger mass adoption since the late 90’s and early 2000’s and had made a large impact on both of our lives and our passion for making as we grew up. Little did we know that due to a combination of our experiences, some of Andy’s unique ideas, some handy grant programs, and lots of gumption and elbow grease, we’d find ourselves starting a company in a literal garage and use this opportunity to finally give back to this community we’d felt so grateful to be a part of.
Shout out to all those who still own an original Mill One!
All these years later, I still try to channel the original ambition we both held back in the day. We thought that within 5 years we’d be able to make a CNC that was so smart and easy to use that you’d only need to click a single button and it would make you your final part, the truest essence of ‘lights out manufacturing’. Of course this would prove much more difficult than we expected, but I’m still so glad that we had a bit of ignorance, essentially, in these early days because every technological effort needs to start somewhere. We also came to better understand that we needed to take more focused steps on our path to that final goal, and this wound up helping us to better understand the other essential parts of a business that make a product work and helps users to feel supported, like:
Committed customer support
Support documents and videos (fun fact, our original Mill One assembly video series was voiced by my father)
Teaching software usage
Providing user inspiration for projects
And all the other parts of an ecosystem that transforms the experience from a transactional purchase to a fully supported journey.
It was a relief then when we finally found our financial footing through the feedback of our early community, who led us toward designing and launching the LongMill on Kickstarter. We’d been quite anxious because after several years it was still a real possibility that we’d have had to throw in the towel due to running very low on cash, and luckily the campaign helped us get back on track.
We were so grateful to see the whirlwind of responses and enthusiasm. I remember being so excited that I was more than happy to spend a late night putting together a video to answer a really common question we’d be getting of “can I use the LongMill vertically?”: https://youtu.be/Kpeo68LFmM0 (fun fact, this became one of our most watched videos over the next couple years, and a couple months later we also had fun standing on the machine while it was running)
How Sienci Has Grown
Skipping from those first 3 formative years to present day, 10 years after we began this whole journey, I can’t help but feel like a proud father who’s watched their child grow up, and look back in fondness despite the arduous journey. Back in the day, the first full-time people that joined our team were pivotal since money was tight and there was lots to do with little margin for error, but it became such a nice flow once we got past 5, then 10, then 20. The extra hands meant we were able to invest so much more time into the things we cared about like higher quality control, more reliable machine availability, and more resources of higher quality to assemble and learn how to use our CNCs. We also we able to allot more budget into much more complex R&D efforts like custom extrusion designs, gSender (to this day, one of my proudest projects I’ve ever undertaken), better electronics, enhanced firmware features, and eventually even larger machines and more complex add-ons like lasers, rotary axes, novel touch plates, and even custom cutting tools. We’re also now a team of almost 60.
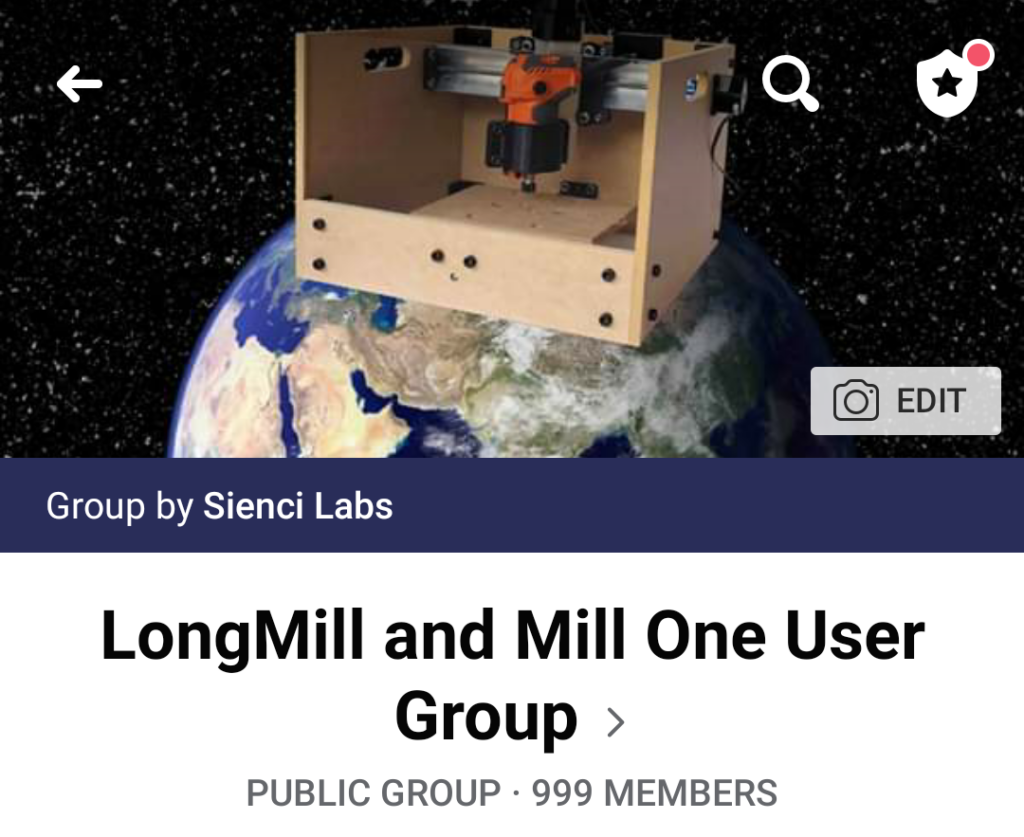
It’s also been amazing to see our great community of CNCers grow alongside us. It’s not typical to have such a helpful group of people all together in one place, and I’m proud to have been joined by many of you in fostering that over the years on both our Facebook group and our Forum. I think it’s great that we can act to not only help those with our machines, but also welcome those from other areas of the CNC community since I’ve always felt that a rising tide lifts all boats. I dug up an old screenshot that I took when I was so excited our Facebook group was about to hit one thousand members, and it’s amazing to see us now past 15k, plus several thousand more on the Forum, and many Github contributors who we’re so happy and grateful to be working alongside. Our community also easily covers the globe now, spanning all continents (except Antarctica) and even some countries I’d never imagined we’d be in including remote islands in the middle of the Pacific ocean!
#image_title
I also want to give a personal shoutout and thanks to some group contributors (and our amazing Forum moderator) who I’ve greatly appreciated chatting alongside through many years in: Grant W, Don R, Jim H, Francis M, Matt M, Bill I, Michael P, Ian G, Heyward O, Bill K, Jeff W, Edwin S, James D, Greg D, Greg C, Jeremy F, Tomek, Tex, John O, Neil F, Ed B, Jens, and Chucky (sorry if I missed anyone else). Anyone who’s been around for a while will probably recognize these individuals for their many contributions toward either answering questions, contributing ideas or code, fending off spam bots, and even bringing some of their own designs to the community; thank you all for all your help along the way, I can say it was a great pleasure working with you.
Other Favourite Parts
I thought maybe I could use the list below as a ‘reflection quick-fire round’ to finish rounding out things that I couldn’t neatly fit into my longer, and perhaps more rambly, prose:
Manually bagging nuts and bolts in our original unheated garage during the Canadian winter (though I don’t know why I look back at it so fondly)
Using our CNCs to cut some of my own, nice home decorations and a camera dolly
Getting gifts from others in the community of projects they made or nice material blanks they wanted to pass along
Seeing our machines go into high schools and universities and maker spaces around the world (as someone who’s always loved to see the improvement and modernization of children’s education)
Getting to work with local Beta tester on all our wacky R&D efforts over the years
Going back to some good ‘ol calculus and geometry to generate a lot of the probing movements and math behind the CAM generation tools in gSender
Launching the SuperLongBoard, alongside all the recent gSender efforts we’d put in, with a lot of effort by the team and to great reception
Seeing all the machine mods and accessories that were released for our machines over the years (including all the unique, personalized dust shoe designs)
Releasing gSender New U, and working toward grblHAL Core feature parity
Celebrating Sienci’s 10 year anniversary with many familiar faces (this was a picture of some of our team from earlier in the year for Halloween)
The Wider Impact I’ve Seen
One thing I forgot to mention earlier is that, though we started Sienci with large ambitions, our underlying goal was to have as big an impact as we could on the hobby CNC space, and I feel confident saying that we’ve done that. This came from a place of what I’d call frustration, knowing what options were out there, how much people were being charged, and how unintuitive many CNCs were to use, we really hoped that we could at least become large enough in the CNC space that others couldn’t help but pay attention to what we were doing and follow-suit with improvements of their own.
All this is to say that I’m going to use this section to brag a little bit and be proud of our accomplishments. Please don’t take what I’ve written here as false attribution or an exhaustive list, this is simply my own list of what I believe to be unique ideas that I feel relatively confident that we either created or popularized in the industry:
Pushing down pricepoint on higher performance
I wouldn’t say we were necessarily the first to do this since much can be owed to projects before us like Shapeoko and OpenBuilds, but I do feel that our presence in the ‘second wave’ continued this push toward faster and higher build quality machines for lower costs.
‘Baseless machines’
A philosophy we helped popularize with the idea being that we could save cost for many shop owners that already had money put into a sturdy table that they could mount the machine to, rather than paying extra for a separate frame, which has since been further adapted by others like Onefinity and FoxAlien.
Focus on strong community collaboration
This one is harder to gage, but I do feel strongly that one of our core company philosophies of keeping a very tight loop between community feedback and the planning of our next steps means that we’ve essentially been able to better empower the CNC community itself into having say over the future of what it wants to see.
Championing open source
We’ve always felt two things, first that people shouldn’t have proprietary lock-in to the hardware or software that they choose to use or spend their money on, and second that if we truly want to keep pushing the hobby CNC space forward then we shouldn’t be scared to share all our work out in the open for others to see and iterate on. The result I feel is a win for everyone, and I hope that more companies in our space would follow suit (though shoutout to other great ambassadors like V1E and Maslow), since we’ve now seen time and again the power and creativity that can come from enabling those within the community to keep moving towards the next steps in technology (something much more visible in the 3D printing space).
gSender
A sending software wasn’t the innovation here, I think it was just the relentless focus on both creating new features that made it feel like the CNC was smarter than it was, while trying to keep it neatly packaged up to be as intuitive as possible. In the early days we certainly got tidbits of inspiration from other senders out there, but I think now that we’ve found our footing it’s been very rewarding to see our novel work and efforts feed back into other senders like UGS, MillMage, ncSender, Genmitsu control, and the Redline controller. I think this will continue to be especially true after our recent 1.5.0 full redesign as there are aspects there that I feel so confident are the future of easier CNCing like our Configuration tab, Helper tool, and Machine Stats, but in the meantime here’s a list of some other specific concepts we brought to the table: touch plate continuity checks, start from line, file stream interruption recognition, seamless incremental-to-continuous jogging, rapid-normal-precise jogging presets, built-in grbl tool-changing support, workaround for full rotary axis control on vanilla grbl CNCs, maintenance reminders, background app waking stops computer falling asleep during cutting, triangle calibration tool, and a recognized CNCs list.
AutoZero
Still to-date the only touch plate I’m aware of that can probe nearly the full spectrum of common cutting tools.
SuperLongBoard
This project had to do with bringing the hobby CNC space into its 32-bit era as well as proving the usefulness of adaption systems that can upgrade older machines, and though there have actually been many that came before us, I do feel that our unique take of offering a user-friendly solution in an open-source and well documented package has been able to progress the concept much further.
Vortex
This is still not a solved issue, but we noticed two issues related to rotary/4th-axes in the hobby CNC space. First is that there’s certainly demand for it, and second is that it’s caught in a chicken-or-egg scenario where machine makers are waiting for easy-to-use software to exist and software makers are waiting for the machines to exist. I felt very proud to be one of the first to break this standstill and make the first step to put out an inexpensive rotary with many novel innovations like the quick-lock tailstock so that we could start to show demand, and we were all so happy once this started more momentum in seeing companies like Vectric be spurred to continue their work on improving rotary handling or Onefinity who followed suit with also releasing a rotary product.
AltMill, AutoSpin, upcoming ATC, and 4×8
This is now me putting the cart a bit before the horse since these are either still new to the market or pending shipping, but I do feel very excited and confident at all the unique things these new offerings will be bringing to the hobby market and really hope their impact will be large and widely felt. Pushing price-to-performance ratio on larger machines, offering essentially a spindle as nearly router prices, building so much more intelligence into a consumer ATC at such a low pricepoint, and bringing a 4×8 into the space also at an amazing pricepoint and still shipped through standard mail are all insane steps and I can’t wait to see what will follow next.
There were also a few other projects that I undertook or lead that maybe weren’t as game-changing but I’m proud to look back on accomplishing:
Co-creating the Mill One and LongMill V1
Leading creation of the LongMill V2, V3, V4, V4b, MK2, and MK2.5
Designing LongMill MK1 dust shoe, MK1 magnetic dust shoe, MK2 magnetic dust shoe, and MK2 dust sheilds
Creating/establishing Sienci’s whole resources documentation system/area, Facebook group, and User Forum
Designing and leading our novel software toolchain suggestion wizard
CAMLab (a foray into simplified, online CAM)
Establishing Sienci’s entire assembly instruction design language, colouring, and look and feel through many iterations over the years along with our approach to long-form, personable videos for assembly, tours, and updates
Thank You
#
Thank you for your trust in us when we were just a couple of people with a dream and a garage full of prototypes. Thank you for your patience when things broke, your excitement when things worked, and your belief that we were building something worthwhile. Thank you for every message, every photo, every project, every suggestion, and every moment you shared. This has been an amazing journey for me and has shaped me as an engineer, as a leader, and as a person.
I’ll carry these memories – both the good and the hard ones – into whatever comes next. Know that though I may be stepping away from Sienci Labs, I’ll always be cheering on each one of you, the continued success of Sienci, and the wider progression of the CNC space as a whole.
If I can also make one final request: if I missed anything in all my above recollections, please do let me know in the comments of anywhere this blog gets posted as I’d love to be reminded of it. Please also share any of your own experiences you’ve had with me, pictures of your setups, or any other way you’ve felt impacted as I’d be very grateful to carry that forward with me as a memento.
Be well, and continue to enjoy making and sharing,
Update Nov 6, 2026: We are still experiencing significant certification and supply chain delays for power supply certification of the AltMill. Our latest estimate for shipping power supplies is January 2027. We deeply apologize for the inconvenience.
We cannot provide one-off power supplies for temporary use at this time. We appreciate your patience as we continue with the certification process.
Update Sep, 2026: We are experiencing significant delays with power supply certification for the AltMill. Our latest estimate for shipping power supplies is December 2026. We deeply apologize for the inconvenience.
We cannot provide one-off power supplies for temporary use at this time. We appreciate your patience as we continue with the certification process.
Original Post: Apr 29, 2026
Ontario Safety Compliance for AltMill and LongMill Machines
Hi everyone, as you guys may know, we had been working with ESA on the safety compliance for the VFDs in 2025, which was eventually completed for sales in Ontario. We are now working with ESA on the compliance for power supplies used in LongMill and AltMill products within Ontario. For customers outside of Ontario, feel free to skip this notice, as this is only limited to within Ontario. If you are within Ontario trying to make an order for the LongMill or AltMill, you may receive a notice at checkout.
Starting April 29th, we’ll be pausing sales for the LongMill MK2.5 and AltMill for customers in Ontario, Canada. Please read further on specific plans for each machine.
LongMill MK2.5
Given that we have a small number of machines left for the LongMill MK2.5, it’s likely that we will be clearing out of this stock before having a prepared power supply. However, the upcoming LongMill MK3 which is expected launch soon, and will be safety compliant for use and sale in Ontario.
AltMill
Since we are expecting to continue production and development of the AltMill, we have been working on a new power supply design around the safety compliance over the last few months. Based on our development timelines, we expect this to be complete around August 2026.
What if I am in Ontario and want to purchase an AltMill or LongMill?
Please contact us directly for additional support as we may be able to provide you with a one off power supply for temporary use that is safety compliant or hold your order until certified power supplies are ready to ship.
After several months of Edge releases, testing, and community feedback, gSender 1.6.0 is here.
This release represents a large step forward for gSender. Much of the work throughout the Edge cycle focused on building out deeper tooling workflows, expanding controller capabilities in order to support newer versions of grblHAL, and improving performance and stability across the application.
A huge thanks goes out to everyone who tested the Edge builds and provided feedback along the way — many of the improvements below came directly from that input.
Below is a look at the biggest changes that made it into 1.6.0.
Firmware Compatibility
This release expands compatibility with newer grblHAL firmware cores. Updates were made across the communication and configuration layers to better align with recent firmware changes and ensure gSender can properly take advantage of all new features in more recent grblHAL versions.
These improvements help maintain compatibility as the grblHAL ecosystem continues to evolve, allowing gSender to work more reliably with newer controller firmware, updated settings structures, and additional capabilities exposed by newer firmware releases.
Performance and Infrastructure Improvements
Several foundational improvements were made for 1.6.0:
Faster Startup Times
Startup performance has been significantly improved in this release.
A number of internal optimizations were made to the application initialization process, reducing the amount of work that needs to happen before the UI becomes usable. These changes include improvements to module loading, background initialization, and general application startup flow.
In practical terms, this means gSender launches noticeably faster, especially on systems where startup time was previously a concern.
For many users the application should now feel much more responsive when opening, getting you connected to your machine and ready to work sooner.
Build System Improvements
The internal build pipeline was updated, resulting in:
Faster development builds
Smaller packaged application size
Improved overall maintainability
Mac silicon version now provided and added signing for both Mac releases
Built-in G-code Editor
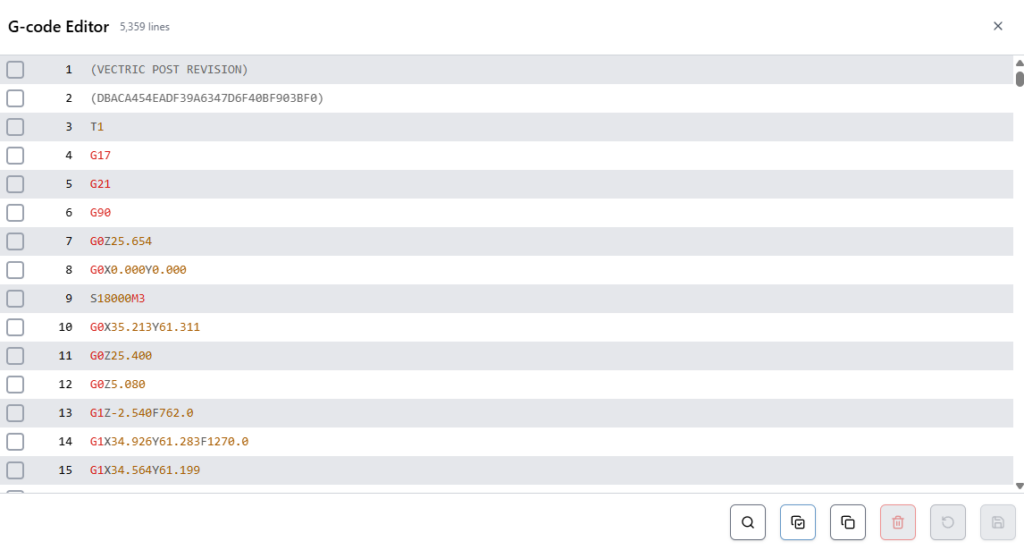
gSender now includes a built-in G-code editor for inspecting and modifying files directly inside the application.
The editor includes:
Syntax highlighting
Search functionality
Quick navigation to specific terms or lines
Basic editing and saving capabilities
The editor also acts as an additional progress indicator while running jobs, highlighting which lines have been processed.
Editor
SD Card File Management
SD card functionality has been expanded significantly.
gSender can now interact directly with files stored on the controller’s SD card for grblHAL devices. It uses yModem protocol for USB connections, and FTP when connected over ethernet.
You can:
View files on the SD card
Upload files
Run files
Delete files
Files can be uploaded using drag-and-drop or file selection, making it easy to move jobs onto the controller.
When running jobs from the SD card, gSender now displays progress feedback similar to streaming jobs directly from the application.
SD Card Tool
Automatic Tool Changer (ATC) Support
One of the largest areas of work this cycle was full ATC workflow support.
gSender now includes an integrated system for managing tools, tracking tool changes, and working with the Sienci ATC more easily.
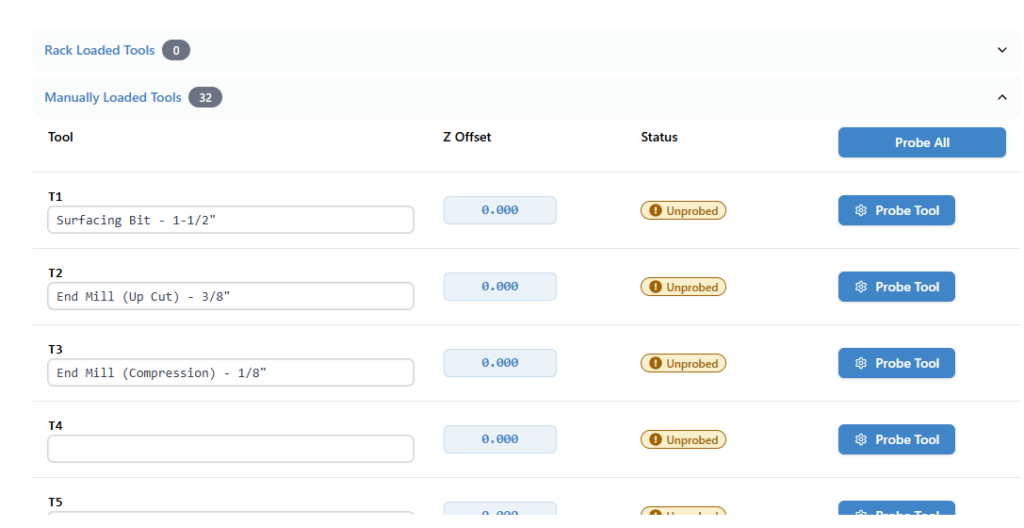
Tool Table
A new Tool Table allows you to manage all tool-related information in one place.
You can now:
Store tool offsets
Assign nicknames to tools
Probe individual tools or complete racks
This makes it much easier to maintain consistent tool setups across jobs.
Tool Table – now with easier nicknames!
Tool Timeline
Tool changes during a job are now represented in a Tool Timeline, giving a clear view of when tool changes occur and which tool is currently active.
This helps users quickly understand multi-tool programs and track job progress more easily.
Tool Timeline
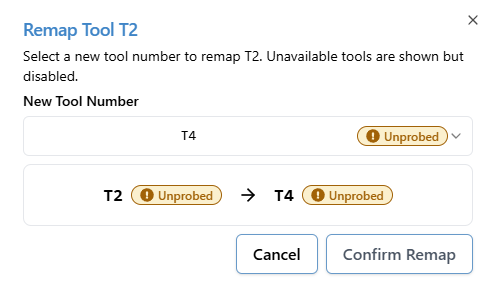
Tool Remapping
Tool remapping allows you to adapt a G-code file’s tool numbers to your machine setup without editing the file itself.
This is particularly helpful when:
CAM tool numbers don’t match rack positions
You want to run the same job with a different tool configuration
Tool racks change between jobs
Remapping can now be configured directly inside gSender before running a job.
Remap Dialog
ATC Workflow Controls
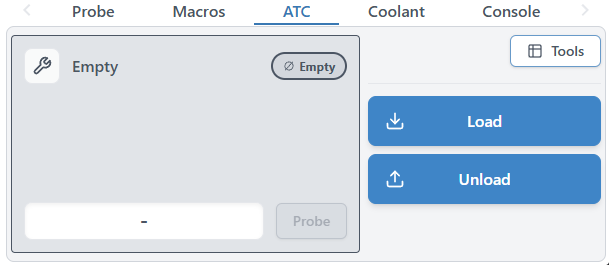
New controls were added to support day-to-day ATC operation.
You can now:
Load tools – both manually and using the rack
Unload tools – both manually and using the rack
These actions tie directly into ATC macros and make managing tool states much easier during operation.
ATC Widget
Accessory Installation Tool
To make getting started with an Automatic Tool Changer easier, gSender now includes an ATC setup tool that helps guide users through the initial configuration process.
The setup tool walks through the core steps required to configure an ATC system, including importing macro templates, defining rack size and behaviour, and writing the required configuration files to the controller’s SD card. This removes much of the manual setup that was previously required and helps ensure the necessary macros and configuration files are installed correctly.
The goal of the setup tool is to simplify the process of bringing an ATC system online, reducing the chances of configuration mistakes and making it easier for users to get up and running with automated tool changes.
We’ve already also implemented a spindle install tool, to help users with setting up their spindle accessory on arrival.
Improved Visualization
Visualization has seen several improvements in this release.
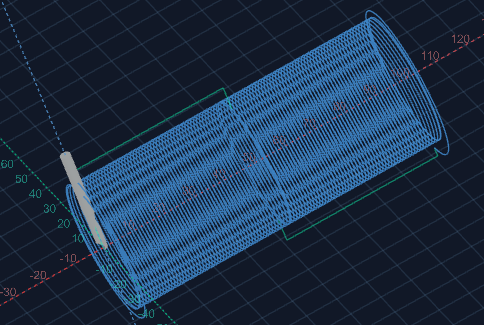
Rotary Visualization Improvements
Rotary jobs are now visualized more accurately, with fixes to geometry rendering and preview alignment. This provides a much closer representation of the final machined result.
Surfacing file no longer two straight lines
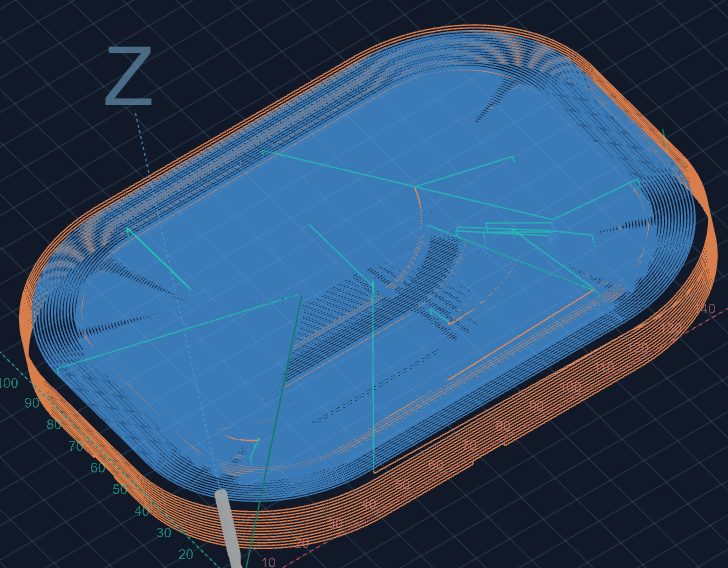
Tool-Based Visualization
Tool changes are now visually separated by colour, making it easier to follow complex multi-tool jobs directly in the visualizer. What colour represents which tool is indicated in the tool timeline.
Toolpath separation
Processed Line Display
A new option allows you to hide processed lines entirely instead of greying them out.
For long jobs this can make the preview significantly easier to read.
Improved visualization speed
Visualization parsing had significant improvments on both speed and memory usage. The end result is that users should be able to visualize larger files faster.
Benchmarks indicate about a 50% increases in visualization and a 35% reduction in memory used.
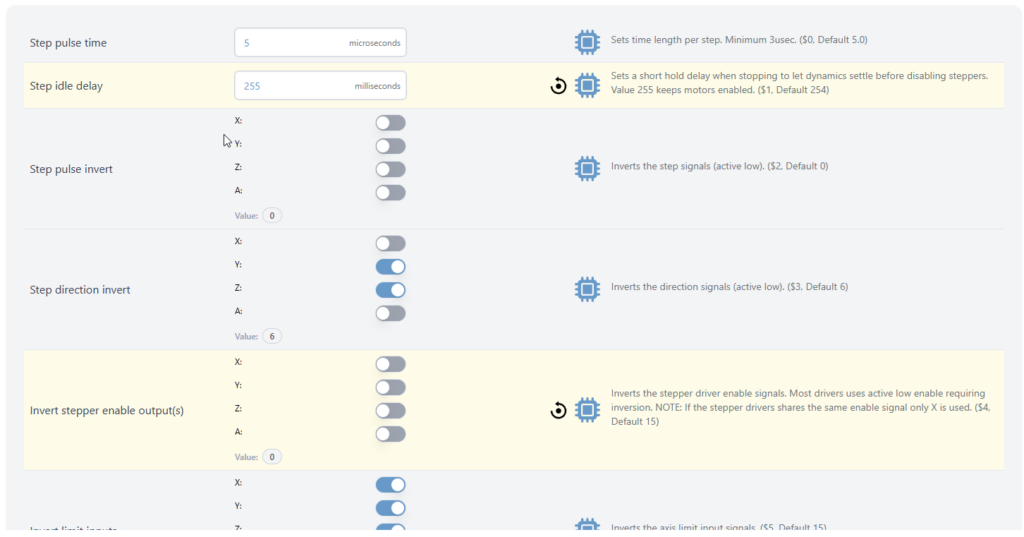
EEPROM Editor
Advanced users now have access to a new EEPROM editor.
This tool allows you to:
View EEPROM values
Modify configuration parameters
Search for specific settings
This replaces the older legacy firmware tool and provides a more flexible interface for working with controller settings. You can find it in the Config section of gSender.
EEPROM tool in Config
Check Mode File Validation
A new Check Mode automation feature makes it easy to validate jobs before running them.
With this option enabled, on job load, you will be prompted if you want to check. If you select yes, gSender will:
Enable GRBL check mode
Run the loaded file
Report any errors found
This helps catch issues before starting a real job.
Additional Improvements
Alongside the major features above, this release also includes a wide range of smaller improvements and fixes.
Some highlights include:
Custom Ethernet ports are now supported
Improved outline behaviour and new outline options (Rapidless square – generate a square that ignores G0 movements and just reflect cutting movements)
Ethernet auto-reconnect improvements
Better portrait mode space usage (larger buttons!)
Remote mode – config is now accessible, settings are now synched between the main app and remote clients
Config tool performance adjustments
Improved job time estimates when feed overrides are active
Improved rotary job time estimation
Option to backup settings over specific time periods.
M0 / M1 pauses now properly display associated comments
Better application responsiveness on small resolutions
Better application responsiveness/use of space on portrait mode
Remote mode configuration access improvements
Updated library dependencies
Numerous bug fixes and stability improvements
Better Config reactivity when updating options that allow new options.
File associations so you can load a gcode file by double clicking it in your file explorer of choice.
Functions that require the machine to have been are disabled until homing is reported by the firmware for grblHAL devices.
Gamepad options and configuration updates – some new behaviours related to jogging.
A number of other behaviour and performance tweaks and fixes
Thank You
This release wouldn’t have been possible without the community members who tested the Edge builds, reported issues, and provided feedback throughout the cycle.
Your input helped shape many of the features and refinements included in 1.6.0.
As always, if you run into any issues or have ideas for improvements, we’d love to hear from you.